PVD Coating Job Shop - Fridley, MN
Anti-Galling Coating for Punches, Dies and Form Tools
Stop metal pickup and scoring on your tooling. Surface Solutions applies PVD hard coatings like Alpha"" and CrN so your tools run with less lubricant.
- Alpha" coating: almost no galvanized build-up vs TiN
- Less lubricant, and no polishing between runs
- Ship tools in from the US, Canada or Mexico
Trusted by Special Tools, Inc. and K&C Manufacturing
Prefer to talk? Call 763-785-9436
Get a quote on anti-galling coating
Tell us about your tooling and what you form. We will recommend the right PVD coating and price your job.
Why shops send galling tools to us
No more base metal pickup
Alpha" coated tooling shows almost no galvanized build-up compared with TiN, so work metal stops sticking to your tool.
Less lubricant, no polishing
Customers run with less lubricant and stop polishing between runs, which cuts steps out of the job.
Longer runs before sharpening
One customer ran 60,000 parts with no sharpening after normally resharpening at 10,000. That is 6x more parts.
Cooler stainless drawing
In a stainless drawing job, CrN coated tooling made over 500 parts that were just warm to the touch, versus 15 parts that were too hot to touch.
Five coatings to match your job
Alpha", CrN, TiN, TiCN and AlTiN/TiAlN. We help you pick the one that fits your material and application.
Ship your tools to us
We are in Fridley, Minnesota and coat work shipped in from across the country, plus Canada and Mexico.
PVD coatings that fight galling and pickup
Galling happens when the work metal welds itself to your tool. A thin, hard PVD film gives the tool a slick, hard surface so the metal slides instead of sticking. That means cleaner parts, less lubricant and fewer stops for polishing or sharpening.
We coat carbide and hardened tool steel tooling for metal formers, stampers, tool and die shops, molders, medical device makers and resharpening services. Tell us the material you run and we will match the coating to it.
- Alpha" proprietary coating - almost no galvanized build-up and reduced chipping of punches
- CrN (chrome nitride) - used in stainless drawing work where tools run hot
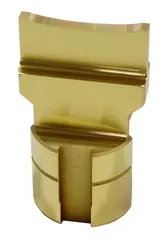
- TiN (titanium nitride) - the classic gold hard coating for tooling
- TiCN (titanium carbo-nitride) for added hardness on punches and dies
- AlTiN / TiAlN for cutting tool life on end mills, drills, taps and inserts
- Applied to carbide and hardened tool steel
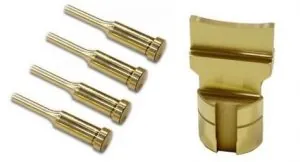
- Punches, dies, draw and form tools, injection molds, blades and wear parts
- Re-coating of manufactured tooling after your shop resharpens it
What customers report after coating
“I just want to say that your Alpha™ coating is amazing. Our operators are not very vigilant at removing the abrasive laser dust and slag but still the coating holds up. Some blocks you alpha coated for me over a year ago are still looking great. Never picks up any base metal and even with minimal lubricant, we can wipe 3/8" thick, grade 80, hot rolled into a tight channel! It seems to get better with more pressure, after a while it becomes a darker brown and gets even slicker. We used to polish a few times a run. Now, with the Alpha™ coating, we have never had to polish, we use less lubricant and have a better looking product. I will continue to use Alpha™ over any of the competitor's coatings due to the durability, price, and your turnaround. Thanks for all your help, you make my job a lot easier!”
“I am continually surprised at how much longer the Alpha coating delays basic sharpening. The attached photos are M4 parts with Alpha coating and they have been in use for over 15 months. My guess is that 15 million parts have been made. They punch thru .057" galvanized steel with a good lubricant. I used to sharpen my uncoated D2 punches every 3 weeks. I have been switching over all die parts from D2 to M4 and then sending for the Alpha coating. When it finally does wear off the M4 immediately shows wear compared to the places the Alpha did not wear off. Those parts are removed – sharpened and sent back to Tincoat and spare coated parts are installed and the die is back in service. I did have one pair of each (one alpha and one TIN) coated round punches running and the Alpha does have almost no galvanized build-up and the TIN has much more. The machine runs one stroke per second for 8 or 16 hours a day with time down for loading coils and breaks. To do maintenance, the die has to be removed: 1 hour, I have to separate the die and sharpen punches and re-assemble – the best case would be 2 hrs if only minimum sharpening needed. Die needs about an hour to install and run again. Also, see the reduced chipping of punches. And longer life on the die because the punch stays sharp and therefore less load/wear on the die. Thanks, Tincoat for reducing my workload and increasing productivity as the dies all run longer without any basic maintenance.”
“In a drawing application (stainless steel), the Alpha™ coated tooling only produced 15 parts and the parts were too hot to touch. Putting CrN on the tool resulted in over 500 parts, with the parts being just warm to the touch.”
What happens after you send the form
Tell us about the tooling
Send the part type, tool material and what you are forming or cutting. Photos of the galling help.
We recommend a coating
We suggest Alpha", CrN, TiN, TiCN or AlTiN for your application and give you pricing.
Ship in, we coat, we ship back
Send the tools to our Fridley, MN shop. We coat them and return them ready to run.
Frequently asked questions
How much does anti-galling coating cost?
Price depends on the coating you choose, the size and number of parts, and how they have to be fixtured. Send your part details and we will quote your job.
Which coating stops galling best?
It depends on the metal you run. Alpha" shows almost no galvanized build-up compared with TiN and stops base metal pickup. In one stainless drawing job, CrN made over 500 parts that were just warm to the touch, while an Alpha" coated tool made 15 parts that were too hot to touch. We help you pick the right one.
Can you coat my tools if I am not in Minnesota?
Yes. We are in Fridley, Minnesota and serve customers nationwide, including Wisconsin and the Upper Midwest, California, New York and Florida, plus Canada and Mexico. Most customers ship tooling in.
What tool materials can you coat?
We coat carbide and hardened tool steel tooling: punches, dies, draw and form tools, injection mold parts, blades, wear parts, cutting tools and medical instruments.
Do you sharpen or regrind tools too?
No. We apply the coating only. You or your sharpening service grinds the tool, then sends it to us for coating or re-coating. Many resharpening shops work with us this way.
How long does coating take?
We aim for reasonable turnaround times. Ask us when you request your quote and we will tell you what the schedule looks like for your job.
Ready to stop galling on your tooling?
Tell us what you run and what is sticking to your tools. We will recommend the right PVD coating and send you pricing. Call 763-785-9436 or use the form.
- Alpha" coating: almost no galvanized build-up vs TiN
- Less lubricant, and no polishing between runs
- Ship tools in from the US, Canada or Mexico
Prefer to talk? Call 763-785-9436